Kurzantwort
Hastelloy X nickel alloy powder is the powder form of UNS N06002, a nickel-chromium-iron-molybdenum solid-solution superalloy that combines outstanding oxidation resistance to 1200 C with good high-temperature strength and exceptional fabricability. Gas-atomized spherical powder is supplied in 15-45 um cuts for LPBF and 45-106 um for EBM, DED, and HIP, with as-built tensile strength of 750-900 MPa and elongation of 30-45 percent. The alloy is one of the most printable nickel superalloys available, with low crack susceptibility and stable parameter windows, which is why it has become a standard material for additively manufactured combustors, turbine vanes, heat-treatment fixtures, and high-temperature chemical processing hardware across aerospace, power generation, and industrial furnace sectors.
| Eigentum | Wert |
|---|---|
| System Legierung | Ni-Cr-Fe-Mo solid-solution superalloy (UNS N06002) |
| Dichte | 8.22 g/cm3 |
| Typische Pulverkorngröße (LPBF) | 15–45 µm |
| Typical Powder Size (EBM/DED/HIP) | 45–106 µm |
| Zugfestigkeit im Fertigungszustand | 750-900 MPa |
| Dehnung im Fertigungszustand | 30-45% |
| Max Service Temperature (oxidizing) | ~1200 C |
| Wesentlicher Vorteil | Best oxidation resistance among printable superalloys, excellent LPBF behavior |
What Is Hastelloy X Nickel Alloy Powder and Its Material Benefits
Hastelloy X nickel alloy powder gehört zur Pulver auf Nickelbasis family and replicates the chemistry of Hastelloy X, a solid-solution superalloy that has served gas turbine combustors and industrial furnace hardware since the 1950s. Unlike precipitation-hardened superalloys that derive strength from gamma prime, Hastelloy X is strengthened by molybdenum in solid solution, and that single design decision explains both its character and its additive manufacturing popularity: with no precipitation phase to crack during printing, the alloy processes on LPBF platforms almost as forgivingly as 316L.
The alloy’s benefits for AM programs include:
- Outstanding oxidation resistance. With 20.5-23 percent chromium, the alloy forms a tenacious protective scale that survives continuous exposure to 1200 C in air, among the highest ratings of any printable alloy.
- Exceptional printability. The solid-solution metallurgy gives low solidification and strain-age cracking susceptibility, wide parameter windows, and high first-pass yield in LPBF production.
- Good high-temperature strength. While not a blade alloy, it sustains useful stress-rupture capability to 900-1000 C, adequate for combustor liners, vanes in less-demanding stages, and furnace hardware.
- Excellent thermal fatigue resistance. The ductile, transformation-free matrix tolerates the repeated heating and cooling cycles that define combustor and furnace duty.
- Deep qualification data. Decades of wrought service plus a growing body of AM-specific data from engine OEM and research programs give designers a solid foundation for part qualification.
The designation appears in several registers: Hastelloy X and HX as trade names, UNS N06002 in procurement documents, 2.4665 in the European system, and GH3536 in Chinese supply chains. The chemistries are close across these names, and purchase specifications should reference the governing standard to avoid disputes over the broad iron and cobalt windows.
The honest limitation is strength at the highest temperatures: above roughly 900 C, precipitation-hardened alloys and single-crystal materials carry far more load, so Hastelloy X is specified for oxidation-limited rather than creep-limited duty.
Chemical Composition and Alloying Element Effects on Properties
The composition balances chromium for oxidation resistance against molybdenum and tungsten for solid-solution strength, with iron providing cost-effective ballast in the nickel matrix.
Chemical Composition of Hastelloy X (UNS N06002)
| Element | Min (wt%) | Max (wt%) | Rolle |
|---|---|---|---|
| Ni | Waage | Waage | FCC matrix; base of oxidation and thermal stability |
| Cr | 20.5 | 23.0 | Forms the protective Cr2O3 scale; primary oxidation-resistance element |
| Fe | 17.0 | 20.0 | Economical matrix diluent; slightly reduces hot strength |
| Mo | 8.0 | 10.0 | Principal solid-solution strengthener; drives high-temperature creep resistance |
| Co | 0.5 | 2.5 | Solid-solution contribution; improves thermal stability |
| W | 0.2 | 1.0 | Supplementary solid-solution strengthener |
| C | 0.05 | 0.15 | Carbide former; contributes creep strength at temperature |
| Mn | – | 1.0 | Deoxidizer residual |
| Si | – | 1.0 | Deoxidizer residual; minor oxidation-scale contribution |
| B | – | 0.010 | Trace grain-boundary strengthener |
| O | – | 0.03 | Powder-quality limit; inclusions harm fatigue and oxidation behavior |
Chromium at this level is what separates Hastelloy X from lower-chromium superalloys such as Hastelloy N: the 20-plus percent content sustains a self-healing oxide scale through long exposures and thermal cycles, which is the property that defines combustor and furnace applications. Molybdenum at 8-10 percent does the structural work, and the combination of high chromium with high molybdenum, difficult to balance in a conventional alloy, is stabilized here by the nickel-rich matrix.
The iron content deserves a word of explanation because it surprises buyers expecting a pure nickel alloy. Up to 20 percent iron substantially reduces raw material cost while barely degrading the properties the alloy is selected for, and this economy is a genuine part of the alloy’s historical success: it delivers near-premium oxidation performance at a mid-tier price point, a positioning that carries through to powder pricing today.
For powder buyers, the carbon window of 0.05-0.15 percent deserves attention: carbon at the low end favors ductility and weldability, while the upper end adds creep strength through carbide formation. Lot certificates should report carbon precisely, and programs qualified on one end of the window should hold subsequent lots close to the qualified chemistry. The broad iron window of 17-20 percent has a milder effect but still shifts density and high-temperature strength at its extremes, which is why serious qualification programs specify tighter internal limits than the headline UNS window.
Physikalische und mechanische Eigenschaften – Vollständiges Datenblatt
The data below consolidate typical values for as-built and heat-treated AM material alongside wrought reference figures, at standard test temperature (23 +/- 5 C) where applicable.
Wichtige Eigenschaften
| Eigentum | Wert | Einheit |
|---|---|---|
| Dichte | 8.22 | g/cm3 |
| Schmelzbereich | 1260-1355 | C |
| Wärmeleitfähigkeit (RT) | 9-11 | W/m·K |
| Wärmeausdehnungskoeffizient (20–1000 °C) | 16-18 x 10-6 | /K |
| Elastizitätsmodul (RT) | ~195 | GPa |
| Yield Strength (RT, as-built LPBF) | 450-600 | MPa |
| Tensile Strength (RT, as-built LPBF) | 750-900 | MPa |
| Elongation (RT, as-built LPBF) | 30-45 | % |
| Yield Strength (870 C, wrought) | 180-220 | MPa |
| Stress Rupture (870 C / 100 MPa, wrought) | >1000 | h |
| Härte (im Auslieferungszustand) | 220-280 | HV |
| Max Service Temperature (oxidizing) | ~1200 | C |
The room-temperature profile is a pleasant surprise to engineers coming from wrought data: as-built LPBF material frequently exceeds wrought tensile strength because the fine cellular solidification structure strengthens the solid solution, while ductility remains excellent at 30-45 percent. A standard solution anneal at 1150-1180 C homogenizes the structure and restores wrought-like properties where design codes require them.
The high-temperature figures define the application space. Stress rupture above 1000 hours at 870 C and 100 MPa covers combustor and furnace duty comfortably, and oxidation testing shows the protective scale remains adherent through thousands of thermal cycles to 1100-1200 C, a performance few printable alloys approach. Creep strength above 900 C, however, falls well short of precipitation-hardened superalloys, and load-bearing parts at those temperatures belong to the Inconel 738 or blade-alloy classes instead.
One aging behavior deserves note for long-service design: extended exposure in the 650-870 C range precipitates carbides along grain boundaries, gradually reducing room-temperature ductility from the annealed values quoted here. The effect is well documented in the wrought literature, design margins account for it in combustor service, and printed material follows the same pattern, so components should be specified against aged rather than as-annealed properties where service time at temperature is long.
Verfügbare Güteklassen – Partikelverteilung und Toleranznormen
Hastelloy X powder is a well-established AM feedstock available from multiple atomization platforms, in fractions matched to each consolidation process.
Verfügbare Spezifikationen
| Parameter | Standard/Wert |
|---|---|
| Partikelgrößenverteilung (LPBF) | 15–45 µm, 15–53 µm |
| Partikelgrößenverteilung (EBM) | 45–106 µm |
| Partikelgrößenverteilung (DED/Ummantelung) | 53–150 µm |
| Partikelgrößenverteilung (MIM) | 0-25 um |
| Sphärizität | >= 0.90 for GA product |
| Scheinbare Dichte | >= 4,3 g/cm³ |
| Zapfstellendichte | >= 5,0 g/cm³ |
| Durchflussmenge in der Halle | <= 16 s/50g |
| Sauerstoffgehalt | <= 300 ppm |
| PSD-Toleranz | D10/D50/D90 certified on every production lot |
| Grad Optionen | Standard N06002; low-oxygen premium grade; PREP grade for HIP rotating parts on request |
| Verpackung | Vakuumversiegelt, mit Argon gespült, 1–50 kg |
The alloy atomizes well and yields a healthy fine fraction, so 15-45 um LPBF cuts carry no unusual premium relative to other superalloy powders, an economic point in its favor against rhenium-bearing or difficult-to-atomize grades. The low-oxygen premium grade serves fatigue-critical combustor and rotating applications, and the PREP grade provides crucible-free cleanliness for HIP-consolidated high-integrity components.
Reuse practice is standard: recycled LPBF powder is refreshed with 30-50 percent virgin material per cycle, with oxygen re-verified periodically, because oxide films on recycled particles degrade both spreadability and as-built density over repeated builds.
Produktionsverfahren: Zerstäubung und Pulverkonditionierung
Production follows the standard superalloy powder route: vacuum-induction-melted heats of virgin raw materials are remelted and converted by Gaszerstäubung (GA) under argon or nitrogen, with argon preferred for the lowest nitrogen pickup in molybdenum-bearing alloys. The alloy atomizes cleanly because its elements are mutually soluble and none is excessively volatile, so chemistry transfer from melt to powder is faithful and lot-to-lot variation is small.
For the highest-integrity applications, PREP production eliminates crucible contact entirely, delivering essentially ceramic-free powder with oxygen at or below 150 ppm, at the cost of a coarser natural distribution and higher unit price.
Post-atomization conditioning follows the established sequence:
- Klassifizierung by sieving and air separation isolates the specified size fractions and removes fines and oversize particles.
- Überprüfung von Durchfluss und Dichte confirms Hall flow rate, apparent density, and tap density against the release specification.
- Chemische Analyse by ICP-OES and inert gas fusion certifies the full element window including carbon, oxygen, and nitrogen content per lot.
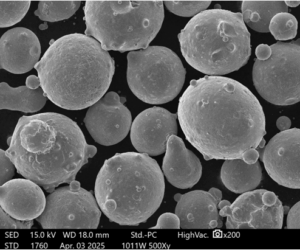
- Morphologische Prüfung by SEM verifies sphericity, satellite content, and overall surface condition.
- Interne Qualitätsprüfung by cross-section metallography or X-ray CT quantifies hollow particle content on premium lots.
- Inertverpackung in argon-flushed, vacuum-sealed containers with desiccant protects the powder through storage and international shipping.
Because the alloy is produced by many suppliers in volume, buyers have unusual leverage to demand lot-level data packages, and competitive qualification of two or three sources is practical, something rarely possible with made-to-order superalloy powders. When comparing sources, the discriminating quality metrics are oxygen content, satellite fraction, and the consistency of the fine-particle tail across lots, since chemistry conformity is generally good across reputable producers while powder-handling behavior varies more than datasheets suggest.
Anwendungen nach Branchen: Automobilindustrie, Elektronik und Luftfahrt
Hastelloy X powder serves the broadest application set of any printable superalloy. Sector context is available on the Anwendungen seite.
Aviation and gas turbines. Combustor liners, fuel nozzles, transition ducts, and turbine vanes in lower-temperature stages are the core applications, and several engine programs now fly printed Hastelloy X fuel nozzles in production. The alloy’s thermal fatigue resistance suits the cyclic duty of these components, and AM consolidation of multi-part nozzle assemblies into single prints eliminates braze joints that were traditional leak and failure points, cutting both weight and assembly cost in one step.
Industrial gas turbines and power generation. The same combustor hardware at longer overhaul intervals drives a large DED repair market, where worn liners and vanes are rebuilt with chemistry-matched powder and returned to service at a fraction of replacement cost. Printed burner components for low-NOx hydrogen-capable combustors are a growth area as power producers transition fuel mixes, and the alloy’s oxidation margin accommodates the higher flame temperatures of hydrogen-rich operation.
Industrial furnaces and heat treatment. Retorts, muffles, radiant tubes, basket fixtures, and conveyor components in carburizing and annealing furnaces exploit the alloy’s 1200 C oxidation rating, and printed thin-wall designs reduce thermal mass and energy consumption relative to cast fixtures while surviving the daily thermal cycles that crack cast alternatives.
Chemical and petrochemical processing. High-temperature reactor internals, catalyst supports, and flare-system components serve in oxidizing environments where stainless steels fail by scaling, with DED repair extending the life of large cast components whose replacement lead times would otherwise idle production units for months.
Automotive and electronics thermal systems. Turbocharger-adjacent hardware, exhaust energy recovery components, and power-electronics cooling structures exposed to high exhaust-side temperatures use the alloy where its oxidation margin justifies cost over stainless alternatives.
Across these sectors, the adoption pattern follows a consistent logic: Hastelloy X is selected when the design temperature exceeds what stainless steels and 718-class alloys survive, but the loads do not justify precipitation-hardened or single-crystal materials. That middle territory is larger in additive manufacturing than in conventional design, because AM’s geometric freedom lets engineers reduce local stresses with conformal cooling and thin-wall features, pulling more components into the alloy’s comfortable operating envelope.
Leistungsvergleich mit alternativen Werkstoffsorten
Selection around Hastelloy X typically benchmarks it against Inconel 625 for corrosion-resistant duty, Inconel 718 for strength, and Haynes 230 for maximum oxidation-resistant performance.
Hastelloy X vs Alternative Superalloys
| Eigentum | Hastelloy X | Inconel 625 | Inconel 718 | Haynes 230 |
|---|---|---|---|---|
| Dichte (g/cm³) | 8.22 | 8.44 | 8.19 | 8.97 |
| Strengthening Mechanism | Solid solution | Solid solution | Precipitation | Solid solution + carbide |
| Max Oxidation Temp (C) | ~1200 | ~980 | ~700 (strength limit) | ~1150 |
| RT Tensile (MPa, as-built) | 750-900 | 850-950 | 1100-1300 | 800-900 |
| Creep Strength (870 C) | Mäßig | Gut | Excellent (to 700 C) | Gut |
| Corrosion Resistance (chemical) | Gut | Ausgezeichnet | Gut | Gut |
| LPBF-Druckbarkeit | Ausgezeichnet | Ausgezeichnet | Gut | Gut |
| Relative Pulverkosten | Mittel | Mittel bis hoch | Mittel bis hoch | Hoch |
Against Inconel 625, Hastelloy X wins on oxidation temperature by roughly 200 C while conceding aqueous corrosion performance, so hot-air duty points to X and chemical-process duty to 625. Against Inconel 718, it concedes strength below 700 C decisively but wins everything above that threshold, where 718 over-ages. Against Haynes 230, it offers comparable oxidation resistance with better availability and lower cost, while 230 holds a strength advantage at the highest temperatures.
The selection rule reduces to environment and temperature: sustained oxidizing service above 900 C with moderate load points to Hastelloy X; maximum strength below 700 C points to 718; aggressive aqueous chemistry points to 625; and the most demanding high-temperature strength-oxidation combinations point to Haynes 230 or the precipitation-hardened class. In practice, many engine and furnace programs qualify both Hastelloy X and one precipitation-hardened alloy, assigning components between them by local temperature, which is why the two powders are frequently sourced together from a single qualified supplier.
Unser Unternehmen
Shanghai Truer Technology Co. Ltd. ist ein in China ansässiger Anbieter von Lösungen für die additive Fertigung, der PREP-Pulverherstellungsanlagen und hochwertige kugelförmige Metallpulver aus einer Hand anbietet. Das 2009 gegründete Unternehmen bietet sowohl Gaszerstäubung (GA) und PREP Fertigungskapazitäten für Nickellegierungen, Titanlegierungen, Aluminiumlegierungen, rostfreie Stähle, Kobaltlegierungen, Kupferlegierungen, Hochentropie-Legierungen und Spezialwerkstoffe.
Truer bietet Dienstleistungen in den Bereichen Entwicklung maßgeschneiderter Legierungen, Prototypenfertigung in Kleinserien sowie Serienproduktion für Branchen wie Luft- und Raumfahrt, medizinische Implantate, Öl und Gas sowie die Automobilindustrie an. Das Unternehmen betreibt in Zusammenarbeit mit führenden Forschungseinrichtungen ein gemeinsames Innovationszentrum für den 3D-Metalldruck.
For inquiries about Hastelloy X nickel alloy powder or other metal powder requirements, Wenden Sie sich an das Team.
FAQ
Q1: What is the typical particle size distribution for Hastelloy X nickel alloy powder? A: LPBF uses 15-45 um or 15-53 um cuts, EBM and HIP use 45-106 um, DED uses 53-150 um, and MIM uses fine fractions below 25 um. The alloy atomizes with good fine-fraction yield, so LPBF cuts are readily available from stock with certified D10, D50, and D90 data per lot.
Q2: Can Hastelloy X powder be used in both SLM and EBM systems? A: Yes, and it is one of the most forgiving superalloys on both platforms. The solid-solution metallurgy avoids strain-age cracking, parameter windows are wide and well documented, and published process data are extensive, making it a common first superalloy for shops entering nickel-alloy printing.
Q3: What certifications does Hastelloy X powder come with? A: Every lot ships with a certificate of analysis covering full chemistry, oxygen and nitrogen content, PSD data, flow rate, and density values. Premium grades add SEM morphology reports and X-ray CT hollow-particle screening, with retained samples for full traceability.
Q4: What is the MOQ for ordering Hastelloy X powder? A: Standard grades are available from 1-5 kg for parameter development and coupon characterization. Production volumes ship in 25-50 kg argon-flushed, vacuum-sealed containers, and the alloy’s multi-source availability keeps pricing competitive relative to made-to-order superalloy powders.
Q5: Can the composition of Hastelloy X be customized? A: Yes. Carbon can be positioned within the specification window to favor either ductility or creep strength, and boron and trace-element levels can be adjusted for specific consolidation routes. Custom melts are produced through the supplier’s alloy development service, typically beginning with a trial atomization batch before campaign volumes.
Q6: What is the typical lead time for Hastelloy X powder orders? A: Stock fractions of standard grade usually ship within one to two weeks of order confirmation. Premium low-oxygen and PREP grades typically require four to eight weeks depending on production scheduling and the certification package required.