簡単な回答
4140 MIM steel powder is a chromium-molybdenum low-alloy steel powder engineered for metal injection molding feedstocks and other fine-powder processing routes. It is chosen when manufacturers need a better balance of strength, hardenability, toughness, and cost than standard plain-carbon steels typically deliver in small, complex parts. Compared with common MIM alternatives such as 4605, 17-4 PH, and 316L, 4140 usually stands out for heat-treatment flexibility, good wear performance, and suitability for structural components where geometry is intricate but mechanical duty is still meaningful.
What Is 4140 MIM steel powder?
4140 MIM steel powder is the powder-metallurgy form of the well-known 4140 chromium-molybdenum steel grade, adapted for injection molding rather than conventional bar, plate, or forging routes. In wrought form, 4140 has long been used for shafts, gears, fixtures, fasteners, and structural machine parts because it combines moderate alloy cost with useful hardenability and a broad heat-treatment window. In MIM form, the same alloy family is reduced to a very fine particle size, blended with binders, molded into net-shape parts, debound, and then sintered to high density.
Why 4140 Exists in MIM Form
The reason to convert a familiar alloy like 4140 into MIM powder is straightforward: many industrial components are too small, too complex, or too expensive to machine efficiently from wrought stock. Metal injection molding is designed for precisely that gap between machining and die casting, especially where part count is high and geometry includes undercuts, thin sections, ribs, holes, or multiple functional surfaces. By using fine alloy powder instead of bar stock, manufacturers can produce near-net-shape parts with reduced scrap and less secondary machining.
Where It Sits in the Steel Family
4140 belongs to the low-alloy chromium-molybdenum steel family. It is not stainless, not tool steel, and not a precipitation-hardening alloy. Its defining feature is a middle-ground chemistry: enough carbon for quench-and-temper response, enough chromium for hardenability and oxidation resistance during processing, and enough molybdenum to support strength and temper resistance without moving into the cost structure of high-alloy systems. That is why it remains relevant in both conventional metallurgy and fine-powder manufacturing.
How 4140 MIM Steel Powder Differs From Wrought 4140
The alloy chemistry may be similar, but the process demands are very different. Wrought 4140 is selected around rolling, forging, machining, and heat treatment; MIM 4140 must also meet requirements for powder fineness, flow under binder loading, sintering response, oxygen control, and dimensional predictability after shrinkage. In practice, a MIM powder supplier is not simply grinding bar stock into powder. The powder has to be produced and classified so that it behaves consistently in feedstock preparation and molding.
Why It Is Not Just Another “Steel Powder”
Many general steel powders are made for press-and-sinter PM, welding, thermal spray, or additive manufacturing, but those routes do not automatically translate into MIM suitability. MIM feedstock needs much finer particle sizes and tighter control over powder shape, interstitial contamination, and agglomeration. That is why fine-particle feedstock quality matters so much: the same nominal 4140 chemistry can perform very differently depending on whether the powder was intended for MIM, conventional PM, or laser-based processes. Standard terminology for additive and powder-based production routes is also formalized in ISO/ASTM 52900 積層造形用語集, which helps buyers distinguish processes that are often grouped together too loosely.
化学組成および材料グレード
Chemically, 4140 is usually described as a medium-carbon chromium-molybdenum steel. In powder form for MIM, the target composition is normally kept within the familiar 4140 range, but the supplier and the part maker may set tighter internal limits to improve sintering consistency, carbon control, and post-heat-treatment response. Those tighter windows matter because very small carbon drift or oxygen pickup can affect both density and final mechanical properties in sintered parts.
Typical 4140 MIM Steel Powder Chemistry
| Grade / Reference | Fe (wt%) | C (wt%) | Mn (wt%) | Cr (wt%) | Mo (wt%) | Si (wt%) | Typical Cross-Reference |
|---|---|---|---|---|---|---|---|
| 4140 MIM steel powder, standard type | バル | 0.38–0.43 | 0.75–1.00 | 0.80–1.10 | 0.15–0.25 | 0.15–0.35 | Closely aligned with AISI 4140 / SAE 4140 |
| Tight-carbon 4140 MIM feedstock grade | バル | 0.39–0.42 | 0.75–0.95 | 0.85–1.05 | 0.15–0.25 | 0.15–0.30 | Internal supplier specification based on 4140 chemistry |
| 4140 PM / fine powder grade | バル | 0.37–0.44 | 0.70–1.00 | 0.80–1.10 | 0.15–0.25 | 0.15–0.35 | Powder-metallurgy adaptation of SAE 4140 family |
| Wrought reference family | バル | 0.38–0.43 | 0.75–1.00 | 0.80–1.10 | 0.15–0.25 | 0.15–0.35 | ASTM A29/A29M alloy steel bars, SAE 4140, EN 42CrMo4, GB 42CrMo |
The table reflects standard industry chemistry expectations rather than one single universal MIM specification. MIM producers often add their own process-control limits for phosphorus, sulfur, oxygen, nitrogen, or residual trace elements because those variables can strongly influence densification and embrittlement risk in small parts.
Grade Equivalents and Practical Naming
In commercial practice, buyers may encounter several naming systems for this alloy family. In North America, AISI 4140 or SAE 4140 is the common reference. In Europe, the closest equivalent is often EN 42CrMo4; in China, 42CrMo is the familiar analogue. These names do not guarantee identical powder behavior, but they do signal the same broader chromium-molybdenum steel family.
Why Carbon Control Is Central
For MIM, carbon is not just another chemistry line item. During debinding and sintering, carbon can move because of furnace atmosphere, binder decomposition, and powder surface condition. If the final carbon level drifts too low, the part can lose hardness and strength after heat treatment; if it drifts too high, distortion or brittle microstructural outcomes become more likely. That is why buyers of 4140 MIM steel powder should request both initial powder chemistry and expected post-sinter chemistry targets.
4140 Versus Neighboring Alloys
Compared with 4130, 4140 generally offers a slightly stronger hardenability-and-strength profile. Compared with 4340, it is less alloyed and usually more economical, though it will not match 4340 in the highest-end strength and toughness combinations. Compared with stainless MIM grades such as 17-4 PH or 316L, 4140 is selected for structural performance rather than corrosion resistance.
技術仕様
Technical specifications for 4140 MIM steel powder begin with the reality that MIM feedstock is much finer than powder used for press-and-sinter PM or most laser deposition routes. A good MIM powder must balance high surface area for sintering with manageable oxidation, acceptable binder loading, and stable rheology during molding. In procurement, that means chemistry alone is never enough; powder size, shape, flow, density, and contamination control all need to be part of the technical sheet.
Typical 4140 MIM Steel Powder Specifications
| Powder Class | Typical PSD Range | 見かけ密度 | タップ密度 | Hall Flow | 酸素含有量 | Sphericity / Morphology |
|---|---|---|---|---|---|---|
| Fine MIM grade | 5–22 µm | 2.8–3.6 g/cm³ typical | 4.2–5.1 g/cm³ typical | Often not reported or limited utility | ≤0.25 wt% typical | Spherical to near-spherical, low agglomeration |
| Standard MIM grade | 10–25 µm | 3.0–3.8 g/cm³ typical | 4.4–5.3 g/cm³ typical | Often conditional due to fine size | ≤0.25 wt% typical | Fine spherical or rounded irregular morphology |
| Broad PM / binder grade | 15~45 µm | 3.2–4.2 g/cm³ typical | 4.6–5.5 g/cm³ typical | 18–28 s/50 g typical | ≤0.20 wt% typical | Good flow, broader distribution |
| Coarser spray or technical grade | 45~105 µm | 3.8–4.8 g/cm³ typical | 5.0–5.9 g/cm³ typical | 15–24 s/50 g typical | ≤0.15 wt% typical | Spherical or irregular depending on process |
These figures are typical commercial reference values, not mandatory global limits. Very fine MIM powders often do not give Hall flow numbers as cleanly as coarser powders, so viscosity under binder loading and feedstock rheology can be more informative than dry-powder flow alone.
4140 MIM Steel Powder for Feedstock Preparation
In MIM, the powder is only one component of a larger feedstock system. The binder package, powder loading, mixing energy, and granulation method all interact with the powder’s morphology. A powder that looks acceptable on a simple certificate may still perform poorly if the size distribution is too broad, the fines are excessive, or the surface chemistry creates instability during debinding. That is why experienced buyers evaluate the powder in relation to the full molding route instead of as a standalone commodity.
Particle Shape and Sintering Behavior
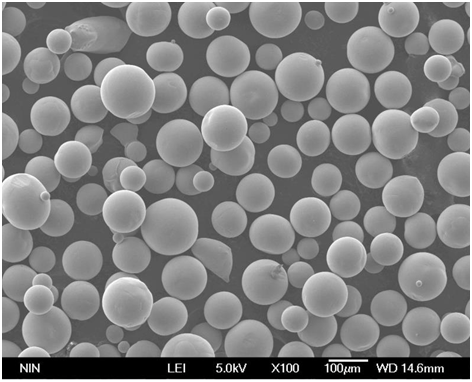
Spherical particles are generally favored for flow and packing, but some MIM formulations deliberately accept a mix of shapes to improve green strength or feedstock behavior. The correct morphology therefore depends on the molder’s process window rather than on a universal preference. Still, for consistent feeding and uniform shrinkage, spherical powder morphology is often viewed as the cleaner starting point.
Oxygen, Surface Area, and Interstitial Risk
Fine powders have higher surface area, which helps sintering but also increases oxidation sensitivity. That makes oxygen and moisture control more important for 4140 MIM feedstock than for coarser conventional PM powders. If the powder has excessive oxide films or poor storage history, debinding and sintering may become more difficult, and heat-treated properties can become less predictable. Guidance from NIST materials measurement programs is often useful when thinking about how powder characteristics affect downstream process stability.
Heat Treatment After Sintering
One reason 4140 remains attractive is its post-sinter heat-treatment flexibility. Depending on part geometry and density, manufacturers may normalize, quench and temper, or use tailored thermal cycles to target a specific balance of hardness and toughness. MIM parts do not behave exactly like wrought bars, but the alloy’s familiar quench-and-temper logic still gives engineers more tuning range than they would get from many simpler steels.
業界を横断した活用事例
The best use cases for 4140 MIM steel powder are parts that combine complex shape with real structural duty. If the component is too simple, machining or conventional PM may be cheaper. If the environment is highly corrosive, stainless grades may be safer. But if the part needs wear resistance, moderate-to-high strength, and geometry that is awkward to machine in large volumes, 4140 often becomes a practical candidate.
Typical Applications for 4140 MIM Steel Powder
| 産業 | Typical Part | AM / PM Process | Why the Powder Is Used |
|---|---|---|---|
| 自動車 | Locking components, sensor housings, actuator parts, small gears | MIM, PM | Strength, heat-treatment flexibility, volume efficiency |
| 産業機器 | Levers, pawls, couplings, precision fixtures, drive parts | ミム | Toughness and wear resistance in compact geometries |
| Power tools and hardware | Trigger mechanisms, structural inserts, fastener components | ミム | Good mechanical performance at moderate alloy cost |
| Consumer technical products | Hinges, brackets, latch parts, compact structural hardware | MIM, secondary machining after sintering | Net-shape complexity with usable strength |
Automotive and Motion Hardware
Automotive and mobility-related subassemblies are natural candidates because they often contain small components with repeating geometry and meaningful loads. These parts may need hardness on contact surfaces but still require some core toughness to survive shock or vibration. 4140 offers a better strength platform than low-carbon steels without forcing a jump into costly specialty alloys.
Industrial Mechanisms and Tooling Adjacent Parts
4140 MIM steel powder is also relevant in industrial machinery, indexing systems, valve hardware, couplings, and compact motion-control mechanisms. Engineers choose it when the part shape is intricate but the service environment is still fundamentally mechanical rather than chemical. Where the duty cycle includes contact, sliding, impact, or repeated loading, 4140 can outperform softer structural grades.
Consumer Durables and Hardware
Some consumer-facing hardware applications do not need stainless appearance or corrosion resistance, but they do need reliable structure in a compact footprint. In those cases, 4140 can be used for hidden mechanical parts where strength and wear performance matter more than decorative finish. The alloy is especially practical when the part will later be coated, blackened, or otherwise surface-finished for protection.
Comparing 4140 With Other Powder Families
Material selection rarely happens in isolation. If corrosion resistance is primary, engineers will compare it with stainless steel powder grades. If weight reduction matters more than raw strength, they may review a titanium alloy powder lineup. If the application is high-temperature rather than structural-at-ambient, nickel superalloy powder options may enter the conversation instead. That comparative step is important because 4140 is a strong general engineering alloy, not a universal answer.
In MIM, the most economical material is rarely the cheapest powder; it is the powder that achieves the target properties with the fewest downstream corrections.
Where 4140 Is Less Suitable
The alloy is not ideal for aggressive corrosion environments, chloride exposure, or applications that require stainless cleanliness. It is also not the easiest route when maximum toughness at the highest strength levels is the main design driver, because more highly alloyed steels may perform better there. Finally, very thin parts with extreme dimensional sensitivity may demand tight process control, since MIM shrinkage and carbon movement both need to be managed carefully.
製造および品質保証
Manufacturing route has a direct effect on how 4140 MIM steel powder performs in molding and sintering. Fine steel powders can be produced through water atomization, gas atomization, or hybrid processing and then further classified for MIM use. The chosen route affects particle shape, oxidation level, tap density, and ultimately the feedstock’s molding behavior.
Typical QA Framework for 4140 MIM Steel Powder
| QA Test | Typical Instrument / Method | Typical Acceptance Focus | なぜ重要なのか |
|---|---|---|---|
| 化学組成 | ICP-OES, combustion analysis | 4140 major elements within target range; residuals controlled | Confirms grade identity and heat-treatment potential |
| 粒度分布 | Laser diffraction, sieve cross-check where applicable | D10/D50/D90 within ordered window | Controls binder loading, shrinkage, and sintering behavior |
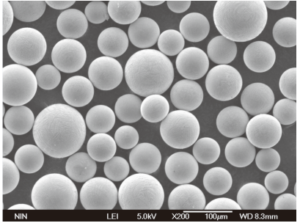
| 形状検査 | SEM and image analysis | Low agglomeration, acceptable shape consistency | Affects feedstock flow and packing |
| Oxygen and carbon testing | Inert gas fusion, combustion analysis | Interstitials within internal MIM limits | Critical for debinding, sintering, and final hardness |
| Density and rheology checks | Apparent/tap density, capillary rheometer or feedstock viscosity | Stable batching and molding response | Predicts production consistency beyond dry-powder data |
Atomization Route and Powder Behavior
Gas-atomized powder is typically favored when high sphericity, cleaner surfaces, and lower oxygen are priorities. Water-atomized powder is often more economical and may sinter well, but it usually has more irregular morphology and higher oxygen levels. For some MIM programs, that tradeoff is acceptable; for others, especially where flow and fine-feature replication are critical, the extra control of gas atomization can justify the cost difference.
Why MIM QA Extends Beyond the Powder Certificate
A certificate of analysis is necessary but not sufficient. 4140 MIM steel powder should also be evaluated in the context of feedstock mixing, injection pressure window, debinding schedule, and sintering atmosphere. If a buyer only verifies powder chemistry and skips rheology or shrinkage studies, qualification risk remains high. This is particularly true for structural parts that must later meet hardness, strength, or dimensional criteria after heat treatment.
Lot Traceability and Reproducibility
For volume production, repeatability matters more than headline values from one successful pilot lot. Buyers should ask about batch numbering, retained samples, storage conditions, packaging atmosphere, and change-control procedures for raw materials and atomization parameters. A trustworthy supply chain for high-density sintering starts with traceable powder lots and a documented route from melt to shipment.
Secondary Operations Matter
Because many 4140 MIM parts are functional rather than decorative, post-sinter operations are often part of the real specification. These may include sizing, machining of critical holes, carburizing alternatives, surface finishing, black oxide, plating, or quench-and-temper cycles. The powder supplier does not perform all those steps, but the supplier should understand how powder characteristics influence them.
なぜサプライヤーとしてTruerを選ぶべきなのか
For buyers evaluating 4140 MIM steel powder, the useful question is whether a supplier understands powder production as an engineering system rather than as a catalog label. That includes melt control, atomization method, particle-size classification, documentation, and the way the powder will be used in MIM, PM, or adjacent additive routes.
Shanghai Truer Technology is relevant in that context because its published capabilities include gas atomization, PREP powder-making equipment, and a broader portfolio of spherical metal powders used in SLM, SEBM, DED, laser cladding, PM, MIM, and HIP. The company background presented on its metal powder manufacturing profile is useful for buyers who want to understand how equipment capability and powder supply are connected in one organization.
ご注文ガイドとサポート
Ordering 4140 MIM steel powder effectively starts with the process, not with the grade name alone. A serious RFQ should state whether the material is intended for MIM feedstock production, pilot-scale molding trials, conventional PM, or another route, because the ideal PSD and morphology can differ significantly. Buyers should also identify whether the part will be heat treated, plated, sized, machined after sintering, or qualified against a specific internal mechanical target.
Typical Ordering Framework
| パッケージング | MOQ Tier | リードタイム | Sample Policy |
|---|---|---|---|
| 100–250 g sealed sample bottle | Lab evaluation | 1–2 weeks typical | Paid sample with basic chemistry and PSD data |
| 500 g to 1 kg inert-packed can | Feedstock development | 2–3 weeks typical | Sample lot for rheology and sintering trials |
| 5 kg vacuum or protected package | Pilot production | 3–5 weeks typical | Retained sample recommended for traceability |
| 20 kg+ industrial lot packaging | Repeating manufacturing demand | 4–8 weeks typical | Batch approval plan commonly agreed before shipment |
What to Include in the RFQ
A strong RFQ will include target PSD, preferred atomization route if known, binder system type, expected powder loading, sintering atmosphere, and the final density or hardness target. If the part will be quenched and tempered, that should also be stated, because heat-treatment intent affects the importance of final carbon control. Including annual volume expectations also helps align sample, pilot, and production-lot strategy.
Sample Qualification Strategy
For 4140 MIM steel powder, sample approval should go beyond chemical review. It is better to run a short program that checks feedstock mixing, molding stability, debinding response, sintered density, shrinkage consistency, and hardness after the intended thermal cycle. Buyers who want to discuss packaging formats, PSD windows, or trial-lot availability can use the powder inquiry contact page.
当社
Shanghai Truer Technology Co., Ltd. was established in 2009 and created its additive manufacturing business in 2019. The company focuses on integrating 3D-printing powder-making equipment and services with 3D-printing powders for engineering applications. Its core technologies include Selective Electron Beam Melting equipment, Plasma Rotating Electrode Process powder-making equipment, and gas atomization-related capability. The powder portfolio includes TiNi, TiTa, TiAl, TiNbZr, CoCrMo, and spherical nickel-based, cobalt-based, titanium-based, copper-based, aluminum-based, and stainless steel powders for use in SLM, SEBM, DED, laser cladding, powder metallurgy, MIM, HIP, cold or hot spraying, welding, and coating across industries including 3C electronics, hand tools, remote control cars, medical, aerospace, and nuclear power.
よくある質問
Q1. Is 4140 MIM steel powder the same as standard 4140 steel?
It is the same alloy family, but not the same product form. MIM powder is much finer and is produced for binder mixing, molding, debinding, and sintering rather than for machining or forging. That difference in form leads to different acceptance criteria for size, oxygen, and morphology.
Q2. What makes 4140 MIM steel powder different from 316L or 17-4 PH MIM powders?
4140 is selected primarily for structural performance and heat-treatment flexibility, while 316L and 17-4 PH are chosen more often for corrosion resistance or stainless-specific requirements. If the application environment is not strongly corrosive, 4140 can offer a more economical route to useful hardness and strength.
Q3. Is gas-atomized 4140 MIM steel powder better than water-atomized powder?
Not in every case, but gas-atomized powder usually provides better sphericity and lower oxygen, which can improve flow and feedstock consistency. Water-atomized powder can still be practical, especially when cost is important and the MIM process window has been developed around it. The best choice depends on molding behavior, sintering results, and final property targets.
Q4. What particle size is typical for 4140 MIM steel powder?
A common MIM range is roughly 5–22 µm or 10–25 µm, depending on the feedstock design and molding strategy. Some suppliers also offer broader cuts for PM or non-MIM uses, but true MIM grades are normally much finer than general-purpose steel powder.
Q5. Can 4140 MIM steel powder be heat treated after sintering?
Yes. That is one of the main reasons engineers choose it. After sintering, 4140 parts are commonly evaluated for quench-and-temper response or related thermal treatments to achieve the target balance of hardness and toughness, though the exact results depend on density and final chemistry.
Q6. What documents should buyers request with each lot of 4140 MIM steel powder?
At minimum, request chemistry, particle size distribution, and oxygen or carbon-related data. For production qualification, it is also sensible to ask for morphology information, lot traceability, packaging condition, and any internal acceptance limits relevant to MIM feedstock preparation and sintering consistency.